SPC: How to Know if a Process is Truly Stable?
What is SPC, how do control charts help identify process changes, and what is the difference between control limits and specification limits? A professional guide to Statistical Process Control.
In this insight you will learn
- SPC helps distinguish between the natural variation of a process and a change indicating a special cause.
- Common Cause Variation is inherent to the process; Special Cause Variation is linked to an exceptional event or change.
- A control chart is used to identify patterns, not just to check if a point has crossed the lines.
- Control limits are derived from the process, while specification limits represent customer requirements—these are two different things.
- A stable process is not necessarily a capable one: stability is assessed before capability (Cp / Cpk).
- SPC enables shifting from asking "Did we produce a defective product?" to asking "Is the process starting to behave differently?"
Not every deviation is a malfunction, and not every result within specification limits indicates that the process is in control. One of the central challenges in quality management is distinguishing between natural variation inherent in a process and a change that signals something in the process has shifted.
Not every deviation is a malfunction, and not every result within specification limits indicates that the process is in control.
One of the central challenges in quality management is distinguishing between natural variation inherent in a process and a change that signals something in the process has shifted.
This is where Statistical Process Control – SPC comes in.
Variation exists in every process
Two products manufactured on the same line, by the same machine, on the same day, will almost never be completely identical.
Variation can stem from raw materials, equipment, operators, environmental conditions, work methods, and other sources.
The question is not whether variation exists.
The question is:
Which variation is part of the normal behavior of the process, and which variation points to a change requiring investigation?
Common Cause and Special Cause
One of the central ideas in SPC is the distinction between two types of variation.
Common Cause Variation is the variation inherent in the process as it currently operates.
In contrast, Special Cause Variation is linked to a specific event or change that is not part of the normal behavior of the process.
For example: a change in raw material, an equipment malfunction, a worn tool, a change in machine settings, or abnormal environmental conditions.
The distinction is important because the response to each type of variation is different.
A control chart is not just a graph
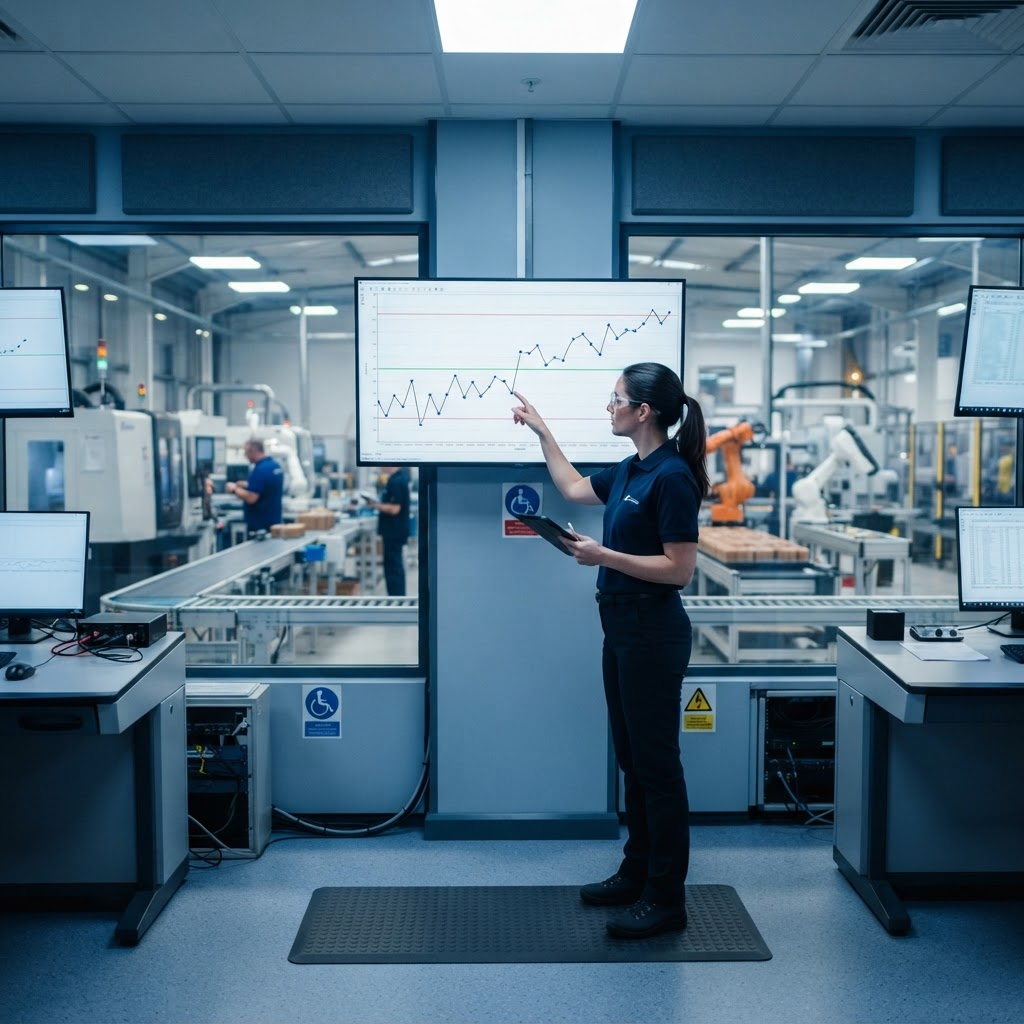
A Control Chart allows you to monitor process performance over time and examine whether there are signs that the process has changed.
The chart typically displays a centerline and statistical control limits.
However, the goal is not just to check if a point has "gone outside the lines."
Certain patterns within the control limits can also provide important information about a change in process behavior.
Therefore, a control chart is a tool for thinking and investigation — not just a graph presented in a report.
Which control charts exist?
Not every control chart is suitable for the same type of data. The choice depends on whether we are measuring a continuous variable or counting items and defects.
- Variables Charts — for continuous data like dimension, weight, or temperature: X̄-R (mean and range), X̄-S (mean and standard deviation), and I-MR charts for individual measurements.
- Attributes Charts — for count data: p and np charts for the proportion and number of nonconforming items, and c and u charts for the number of defects per unit or unit area.
The correct choice is part of the methodology: a chart unsuitable for the data may generate false alarms — or miss a real change.
Pattern recognition rules
A point outside the control limits is only one of the possible signs.
Accepted detection rules — such as Western Electric rules and Nelson rules — also address patterns within the limits, for example:
- A single point beyond a control limit.
- A number of consecutive points on the same side of the centerline.
- An increasing or decreasing trend across several consecutive points.
- Many points clustering near the control limits.
Such rules increase sensitivity to change — and simultaneously increase the number of false alarms, so it is important to define in advance which rules to implement and how to respond to an alert.
Control limits are not specification limits
This is one of the most important distinctions in SPC.
Specification Limits represent the requirements that the product or process must meet.
Control Limits are derived from the statistical behavior of the process.
These are two different things.
It is possible that all measurements are within specification, but the process shows a statistical sign that something has changed.
Conversely, a process may be very stable — but its mean or dispersion may not allow for consistently meeting specification requirements.
Stability is not capability
A stable process is a process whose behavior is relatively predictable from a statistical perspective.
But that does not mean it is capable of meeting customer requirements.
This is where Process Capability comes in: Cp and Cpk indices examine the relationship between process performance and specification limits, and they are discussed in depth in the dedicated knowledge base on process capability.
Therefore, it is correct to think in this order:
First, understand if the process is stable — then examine its capability to meet requirements.
An example from industry
Suppose a production line measures a critical characteristic every hour.
All results are still within specification limits, so, seemingly, everything appears normal.
However, the control chart points to a gradual trend in one direction.
An investigation reveals that a tool in the process is gradually wearing down.
Without statistical monitoring, the organization might only have discovered the change after the first product exceeded the specification.
SPC enables a shift from an approach of:
"Have we already produced a defective product?"
to an approach of:
"Is the process starting to behave differently?"
SPC is not just for the Quality Department
When SPC works correctly, it is not a tool that belongs only to the quality engineer.
The data can be used by production, engineering, operations, and process improvement personnel to understand how the process behaves and to make decisions based on facts.
The goal is not to produce more charts.
The goal is to identify a change in time and act before it becomes a significant problem.
And what is the connection to AI?
As production systems generate more data, it is possible to integrate advanced tools for detecting patterns and anomalies.
AI can assist in analyzing large amounts of information and highlighting events for review.
But even in an advanced world of Analytics and AI, the statistical principles remain important.
A system can identify a pattern — but one still needs to understand what it means for the process and whether action is required.
In conclusion
SPC allows an organization to understand the process and not just inspect the product at the end.
By monitoring variation, using control charts, and distinguishing between common and special causes, changes can be identified earlier and data-driven decisions can be made.
The goal is not to wait for a specification deviation. The goal is to recognize that the process is changing before the deviation becomes a failure.
Want to deepen your knowledge of SPC, statistics, and process improvement?
SPC is one of the professional topics covered in the CQE – Certified Quality Engineer track of the ALD Academy.
Before building a control chart — it is worth ensuring that the measurement itself can be trusted: MSA and Gage R&R
Insight from Dr. Zigmond Bluvband
“Quality is not created in the final inspection. It is created in the decisions made at the beginning of the project.”
This insight is based on professional knowledge, practical experience and study materials of ALD Advanced Solutions, and inspired by the books and publications of Dr. Zigmond Bluvband.