MSA and Gage R&R: Can We Trust Our Measurement System?
What is MSA, what does Gage R&R evaluate, and what is the difference between Repeatability and Reproducibility? Here is how to determine if a measurement system is reliable and if its data can be trusted.
In this insight you will learn
- What is MSA and why is it important before analyzing quality data
- What is the difference between product variation and measurement system variation
- What does Gage R&R examine
- What is the difference between Repeatability and Reproducibility
- How an unsuitable measurement system can lead to incorrect decisions
- Why calibration alone is not always enough
Before making a decision based on data, it is worth asking one fundamental question: Can you trust the measurement that produced it?
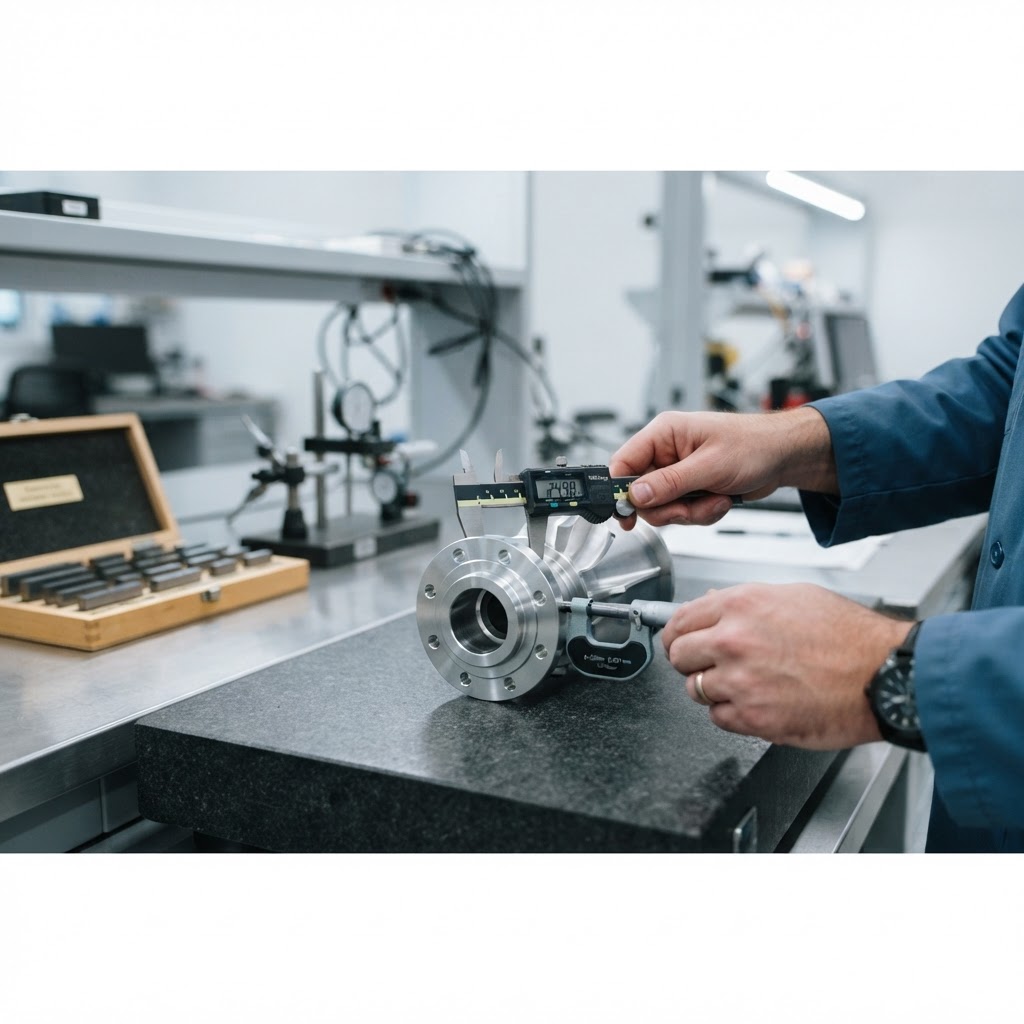
In quality processes, we measure constantly: dimensions, weight, temperature, pressure, performance, electrical characteristics, and more. Significant decisions are made based on these measurements: Is the product compliant? Does the process meet requirements? Is a change necessary? Is there an out-of-specification condition? However, there is a point that is sometimes overlooked: The measurement process itself is a process — and it also contains variation. ## What is MSA? MSA (Measurement System Analysis) is an approach for analyzing the ability of a measurement system to provide suitable information for decision-making. When we say 'measurement system,' we are not referring only to the instrument. The measurement system can include the instrument, the measurement method, the person performing it, environmental conditions, the fixture for the item, the software, the resolution, and the procedure by which the data is collected. Therefore, even a high-quality and calibrated instrument does not necessarily guarantee that the entire measurement process is fit for purpose. ## Why check the measurement system at all? Suppose we measure a critical characteristic of a part several times and receive a slightly different result each time. The question is: Is the part actually changing — or is the measurement system creating some of the variation we see? If we cannot answer this question, it is difficult to know how much we can trust the data for process control and decision-making. A measurement system with high variation can lead to two types of errors: * A compliant product might appear non-compliant and be rejected. * Conversely, a product that does not meet requirements might appear compliant and continue through the process or reach the customer. In both cases, the cost can be significant. ## Gage R&R – Where does measurement variation come from? One of the well-known tools within MSA is Gage Repeatability and Reproducibility – Gage R&R. The analysis focuses on two central sources of variation. ### Repeatability Does the same operator, using the same equipment and the same method, receive consistent results when measuring the same item multiple times? ### Reproducibility Do different operators receive similar results when they measure the same items using the same measurement system? This distinction is important because it helps to understand whether the source of variation is primarily related to the equipment, the way it is used, or the differences between operators. ## Industry Example Suppose several employees measure the diameter of a component as part of an acceptance inspection. The parts are near the specification limits, and different decisions are made by the employees regarding the same parts. At first glance, one might think the problem is in the production process. But a Gage R&R study might show that a significant portion of the variation actually comes from the measurement process. In such a case, changing the production process will not necessarily solve the problem. It may be necessary to improve the measurement method, the way the part is fixed, the equipment, or the training of the operators. ## But the instrument is calibrated. Isn't that enough? Calibration is a very important component in measuring equipment control, but it answers a different question. Calibration provides information about the instrument's performance relative to a defined reference under specific conditions. MSA examines the measurement system in the context where it is actually used. Therefore, it is possible for an instrument to be calibrated and yet the measurement system is not sufficiently suitable for a specific need. ## MSA before SPC The connection between measurement and process control is especially important. If we want to perform SPC and analyze the variation in the process, but the measurement system itself adds significant variation, we might misinterpret the data. In simple words: Before trying to control the process using data, one must ensure that the data itself is fit for use. ## MSA is not just a requirement It is easy to turn a measurement system study into just another document that needs to be completed. But its real value is in decision-making. When we know how reliable and fit-for-purpose the measurement system is, we can better distinguish between a real change in the product or process and 'noise' created in the measurement process. ## Summary Data is the basis for many quality decisions. But seemingly accurate data is not necessarily data that can be trusted. MSA and Gage R&R allow an organization to examine the measurement system itself, understand the sources of variation, and improve the quality of the information upon which decisions are based. Before asking what the data says — it is worth ensuring that the measurement system knows how to tell us the truth. ### Want to delve deeper into measurement tools, statistics, and quality engineering? MSA and Gage R&R topics are integrated within the CQE – Certified Quality Engineer track at ALD Academy. Want to also understand how to control the process itself? SPC – Statistical Process Control For a professional consultation with the ALD team
Insight from Dr. Zigmond Bluvband
“Quality is not created in the final inspection. It is created in the decisions made at the beginning of the project.”
This insight is based on professional knowledge, practical experience and study materials of ALD Advanced Solutions, and inspired by the books and publications of Dr. Zigmond Bluvband.