Process Capability Cp and Cpk – Why a Stable Process Doesn't Necessarily Meet Requirements
What is the difference between a stable process and a capable process? Learn about Cp and Cpk, how to interpret them, and why stability should be verified before calculating capability.
In this insight you will learn
- The difference between a stable process and a capable process
- What Cp measures and what it misses
- What Cpk measures and why it is the practical metric
- What the gap between Cp and Cpk reveals
- How to interpret accepted Cpk values
- Why process stability must be checked before calculating capability
Process capability **Cp and Cpk** – why does a stable process not necessarily meet requirements?
Not Every Stable Process is a Capable Process
Assume a manufacturing process produces a component, all measurements are within specification limits, and the process appears stable over time.
At first glance, everything looks fine—but statistical stability is not a guarantee that the process is capable of meeting requirements over time.
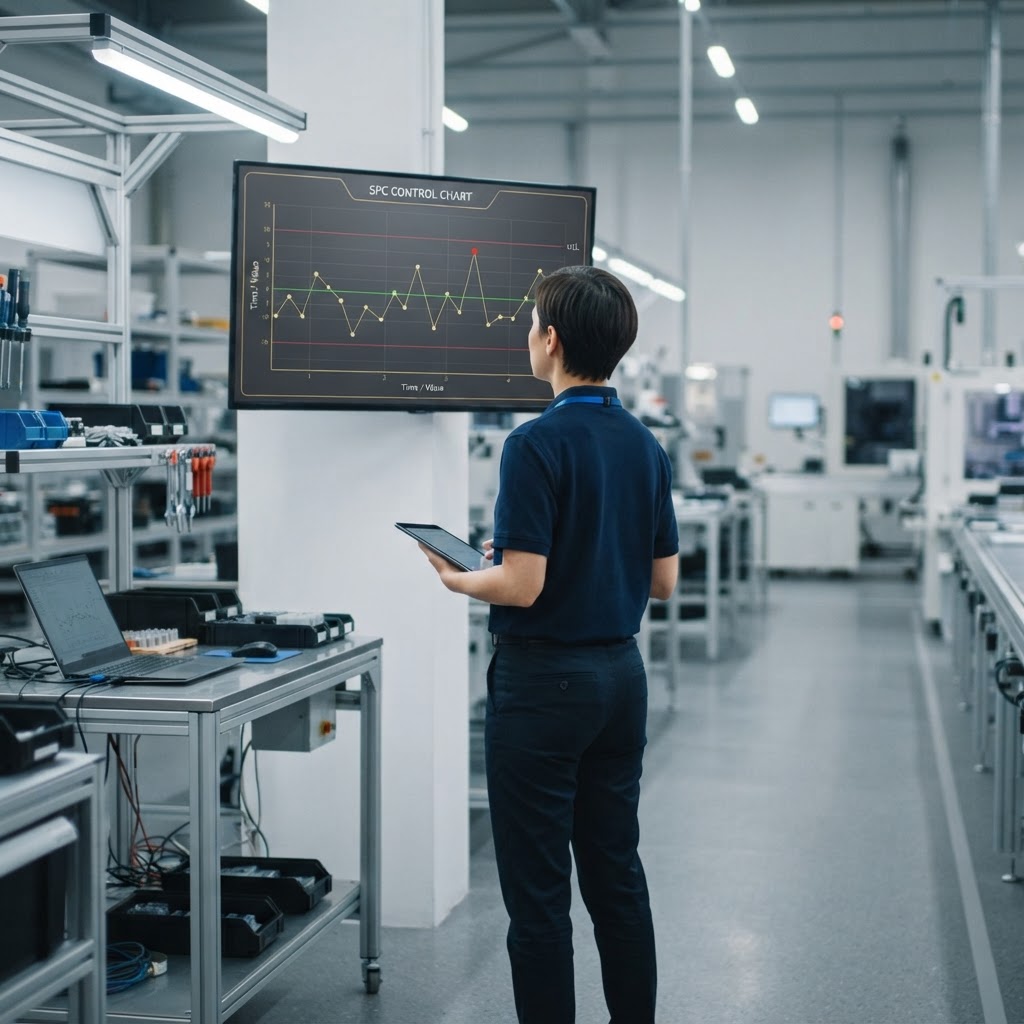
Before calculating process capability, it is important to understand what Statistical Process Control (SPC) is, how to read a control chart, and the difference between common cause variation and special cause variation—all this foundation can be found in SPC and Control Charts Knowledge Base.
Why Can a Stable Process Still Fail?
A stable process is one whose behavior is relatively predictable from a statistical standpoint.
However, stability describes the natural variation of the process—not its position relative to requirements.
If the natural variation of the process is large relative to the specification width, or if the mean is close to one of the limits, the process may consistently produce defects—even though it is perfectly stable.
What is Cp?
Cp (Process Capability) examines the ratio between the specification width and the width of the process's natural variation.
Cp = (USL − LSL) / 6σ
The higher the Cp, the greater the margin between the natural fluctuation of the process and the specification limits.
But Cp ignores the position of the mean relative to the center of the specification. A process can show a high Cp—and still produce defects—if it is poorly centered.
What is Cpk?
Cpk takes into account both the variation and the location, which is why it is the more practical metric for most decisions.
Cpk = min[(USL − μ) / 3σ , (μ − LSL) / 3σ]
A high Cpk indicates that the process is both stable and centered relative to the specification, with a sufficient margin for both limits.
When Cp is high and Cpk is low, the gap between them almost always points to a centering problem—not a variation problem.
How to Interpret the Numbers?
Common industry values:
- Cpk < 1 — The process is not capable of meeting requirements consistently
- Cpk ≈ 1.33 — An acceptable level of capability for many requirements
- Cpk ≥ 1.67 — High capability, suitable for stringent requirements or regulated industries
Numbers are not a substitute for judgment: customer requirements, standards, the criticality of the feature, and the level of risk determine what is required.
The Right Order: First Stability, Then Capability
One of the most common mistakes is to calculate Cpk, see a number that looks good, and end the analysis.
But if the process is not stable, the data does not necessarily describe constant and predictable behavior, and capability metrics may be misleading.
The correct order is:
Measure → Examine stability → Identify special causes → Stabilize the process → Examine capability → Improve.
This is how statistics turns from a reporting tool into a management tool.
Don't React to Every Fluctuation
In every process, there is natural variation.
If you re-adjust the machine every time a small change in measurement appears, you might actually introduce additional variation into the process—and hurt its capability.
The quality engineer's challenge is not to eliminate every fluctuation—but to understand when it is natural noise and when the data signals a real change.
In Summary
Process capability is the tool that connects the statistical stability of the process to the product requirements.
Cp describes the potential relative to the specification width, Cpk adds the mean's location—and both are only valid when the process is stable.
A stable process that cannot meet requirements is not a statistical problem—it is an engineering problem that requires a change to the process itself.
Further Reading
SPC and Control Charts – How to Identify a Change in the Process?
The Seven Quality Tools Every Organization Should Know
CQE Course – Certified Quality Engineer
Want to Deepen Your Knowledge of Process Capability, Cp, and Cpk?
These topics are integrated into the ALD Academy CQE program as part of the practical tools for quality engineering.
Insight from Dr. Zigmond Bluvband
“Quality is not created in the final inspection. It is created in the decisions made at the beginning of the project.”
This insight is based on professional knowledge, practical experience and study materials of ALD Advanced Solutions, and inspired by the books and publications of Dr. Zigmond Bluvband.