The Bathtub Curve – What It Says About Early, Random and Wear-out Failures
The bathtub curve describes how the failure rate of a product population changes over its life. What each of its three regions means, what to do at each stage, and when this familiar model misleads.
In this insight you will learn
- What the bathtub curve describes, and why it refers to a population rather than to a single unit
- What causes early failures, and how to handle them with ESS and burn-in
- Why useful life is the basis for assuming a constant failure rate and for MTBF
- How to identify the onset of wear-out and plan preventive replacement
- When the bathtub curve does not describe reality, and what to do instead
The bathtub curve (Bathtub Curve) is one of the most familiar graphs in reliability engineering. The horizontal axis represents time (or operating hours, cycles, kilometres), and the vertical axis represents the failure rate – in professional terms, the Hazard Rate: the probability that a unit that is still working will fail in the next unit of time.
What Does the Bathtub Curve Describe?
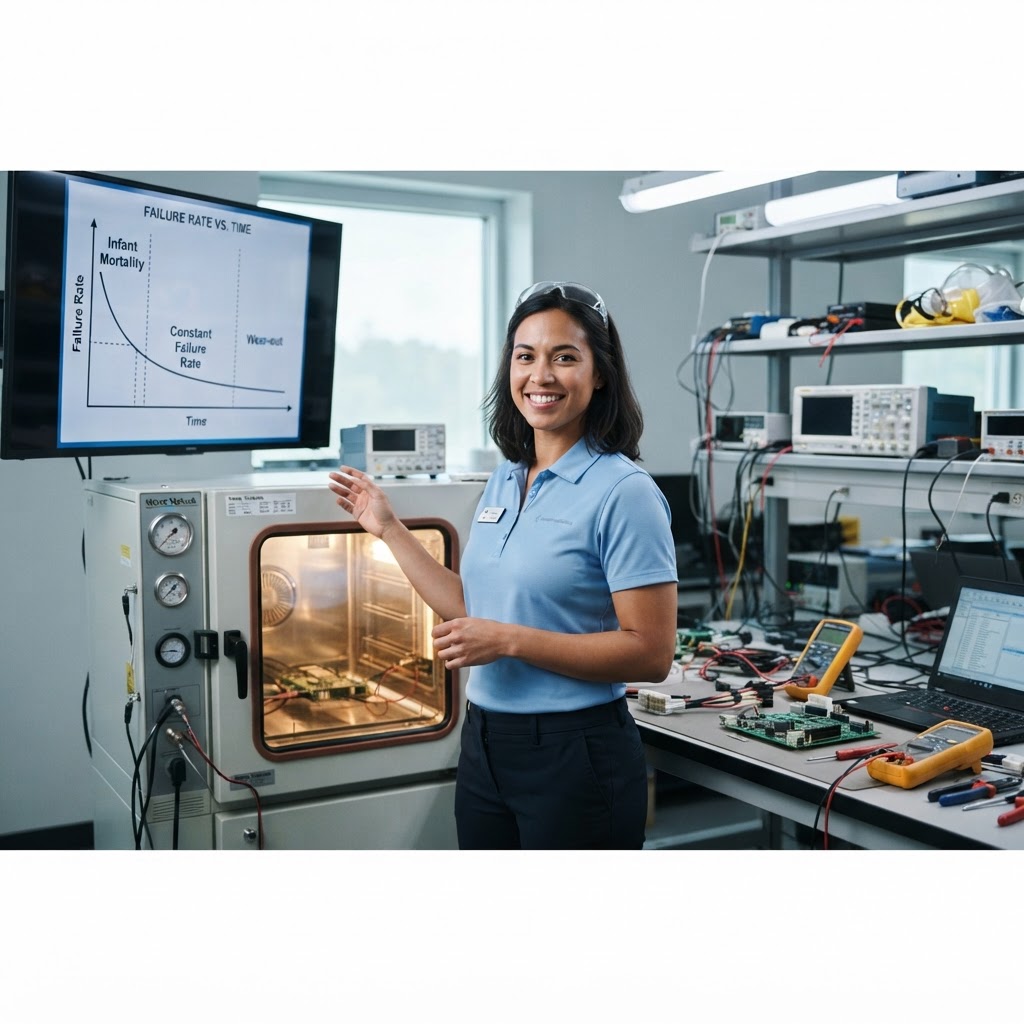
The bathtub curve (Bathtub Curve) is one of the most familiar graphs in reliability engineering. The horizontal axis represents time (or operating hours, cycles, kilometres), and the vertical axis represents the failure rate – in professional terms, the Hazard Rate: the probability that a unit that is still working will fail in the next unit of time.
The curve has three regions, hence its name:
- Infant mortality – a high failure rate at the start, which steadily declines.
- Useful life – a low and relatively stable failure rate.
- Wear-out – a failure rate that rises as the product ages.
A point worth understanding from the outset: the curve describes a population of units, not an individual unit. It does not say when a particular device will fail, but rather how the failure mechanisms of all the units behave together over time. In practice, the curve is the sum of several different mechanisms that overlap one another.
Why does this matter? Because each region of the curve points to a different kind of problem, and therefore to a different action. An early failure points us to manufacturing and suppliers, a random failure points to design and safety margins, and a wear-out failure points to the maintenance plan and service life. An organization that does not know which region its problem sits in may invest in the wrong place: adding tests when the problem is in design, or replacing components when the problem is in manufacturing.
Region One: Early Failures
At the beginning of life, the units that fail are mainly those that left production with a latent defect: a weak solder joint, contamination, a faulty component from a supplier, an assembly error or handling damage. These units are "weak" to begin with, and therefore they fail quickly. As they drop out of the population, the units that remain are stronger, and the failure rate declines.
In Weibull analysis, this region is expressed by a shape parameter β smaller than 1.
What to do here:
- Treat the root cause – process control, supplier quality and assembly control. An early failure is almost always a sign of a problem in production quality or in the supply chain, not in design.
- ESS – Environmental Stress Screening – exposing the units to temperature cycles and random vibration before shipment, so that latent defects are revealed in the factory rather than at the customer's site.
- Burn-in – operating the units for a defined period, usually at elevated temperature, in order to "screen out" the weak ones.
Two important caveats. First, screening costs money and time, and if it is too aggressive it may also consume part of the life of the good units. Second, screening treats a symptom: every failure it reveals must feed a root cause analysis, so that the defect is not created in the first place. Screening with no feedback loop behind it becomes a permanent cost.
Region Two: Useful Life
In this period the failure rate is low and relatively stable. Failures are caused mainly by random events – an abnormal electrical load, impact, extreme environmental conditions or misuse – and not by ageing. In Weibull analysis this is the case where β is close to 1, that is, an exponential distribution.
This is the region in which MTBF is defined in the classic sense. When the failure rate λ is constant, MTBF equals 1/λ. The older reliability prediction methods, such as MIL-HDBK-217F, also assume constant component failure rates.
And from this follows a practical conclusion that surprises quite a few managers: during useful life, preventive replacement does not improve reliability. If the failure rate is constant, a new unit is no safer than a unit that has already been running for two years. Here reliability is improved through design: design margins, derating (operating components below their maximum values), redundancy and protection against overload stresses.
Region Three: Wear-out
At a certain stage, ageing mechanisms begin to act: material fatigue, corrosion, wear of bearings and moving parts, drying of electrolytic capacitors and fatigue of solder joints under temperature cycles. The failure rate rises with time, and in Weibull analysis this is β greater than 1.
What to do here:
- Define service life – until when the product or component is expected to operate.
- Plan preventive replacement before wear-out begins. Here, unlike in the second region, replacement has real value.
- Monitor condition (Condition Monitoring) – vibration, temperature or electrical parameters – where deterioration can be identified before failure.
B-life values from Weibull analysis, for example B10, help set the replacement interval on the basis of data rather than on the basis of a gut feeling.
A Practical Example
A manufacturer of power supplies for industrial systems consolidated its field return data in a FRACAS system, and analysed each failure mechanism separately.
In the first months after shipment, most returns came from defective solder joints and from connectors that had not been properly locked – a clear picture of early failures. The team corrected the soldering process and added temperature-cycle screening before shipment, and returns of this kind declined.
After several years of operation, a different kind of failure began to appear: fans whose bearings had worn out and electrolytic capacitors that had dried out. Weibull analysis showed β greater than 1 – wear-out. The response was entirely different: preventive replacement of the fan was defined as part of the periodic service, and in the next design, capacitors with a higher temperature rating and longer life were selected.
The lesson: each region required a different action. A single MTBF figure for the whole product would have hidden both stories.
When the Bathtub Curve Misleads
The bathtub curve is an excellent teaching model, but it is not a law of nature.
- Not every item behaves like a bathtub. The research by Nowlan and Heap at United Airlines, on which the RCM approach rests, identified six different failure patterns in aircraft items. The classic bathtub pattern was found in only a small minority of items, and many complex items showed no clear wear-out region at all.
- Maintenance can add early failures. Disassembling and reassembling a system that works well can introduce new defects, and return the system to the start of the curve.
- Mixed mechanisms hide the picture. An aggregated product curve can look flat even when a wear-out mechanism and an early-failure mechanism are hidden beneath it. That is why each failure mode is analysed separately.
- Do not assume a constant failure rate without data. The assumption is mathematically convenient, but if it is wrong, both the maintenance plan and the availability calculations will be wrong.
In Summary
The bathtub curve teaches that the failure rate has an "age", and that this age determines what the right thing to do is: at the beginning of life we address production quality and screening, during useful life we improve the design, and at the wear-out stage we plan preventive replacement and condition monitoring.
But the curve is a starting point, not an answer. The way to know which region each failure mechanism is in is to collect field and test data, analyse it, and test the assumptions against reality. Whoever manages maintenance or reliability by the bathtub "on autopilot" may replace components that there is no reason to replace, and miss wear-out that is approaching.
Further Reading
Weibull Analysis – What Does the Failure Distribution Say About Your Product?
MTBF – What Does the Number Really Mean, and What Does It Not?
CRE Certification Preparation Course
Want to Go Deeper?
Life data analysis, failure rate models and reliability-based maintenance planning are part of the CRE body of knowledge (ASQ). ALD Academy's preparation course prepares candidates for this certification.
This insight is based on professional knowledge, practical experience and study materials of ALD Advanced Solutions, and inspired by the books and publications of Dr. Zigmond Bluvband.